
TECHFLOW at 11th IMRC 2024: A Successful Showcase of Innovation and Expertise
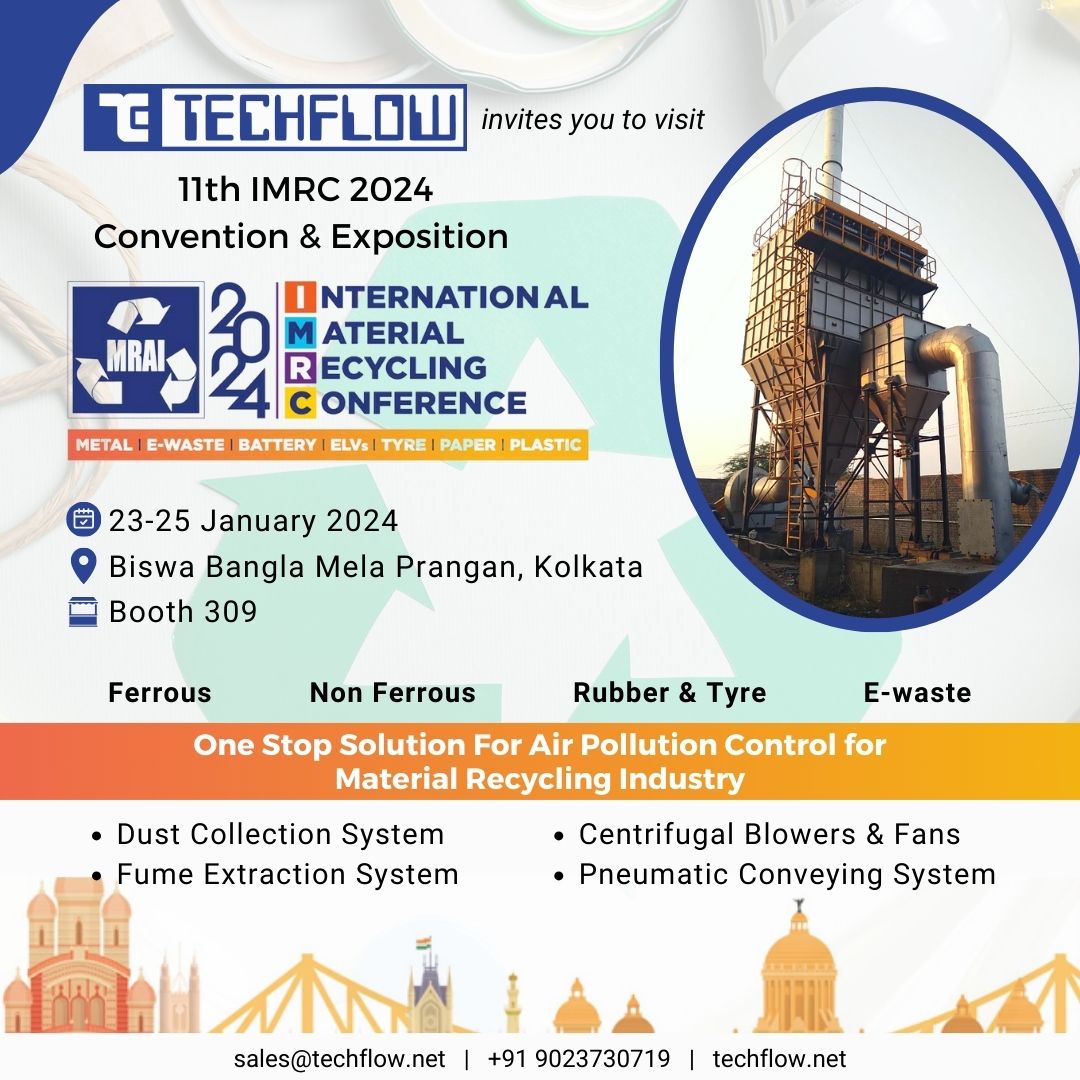
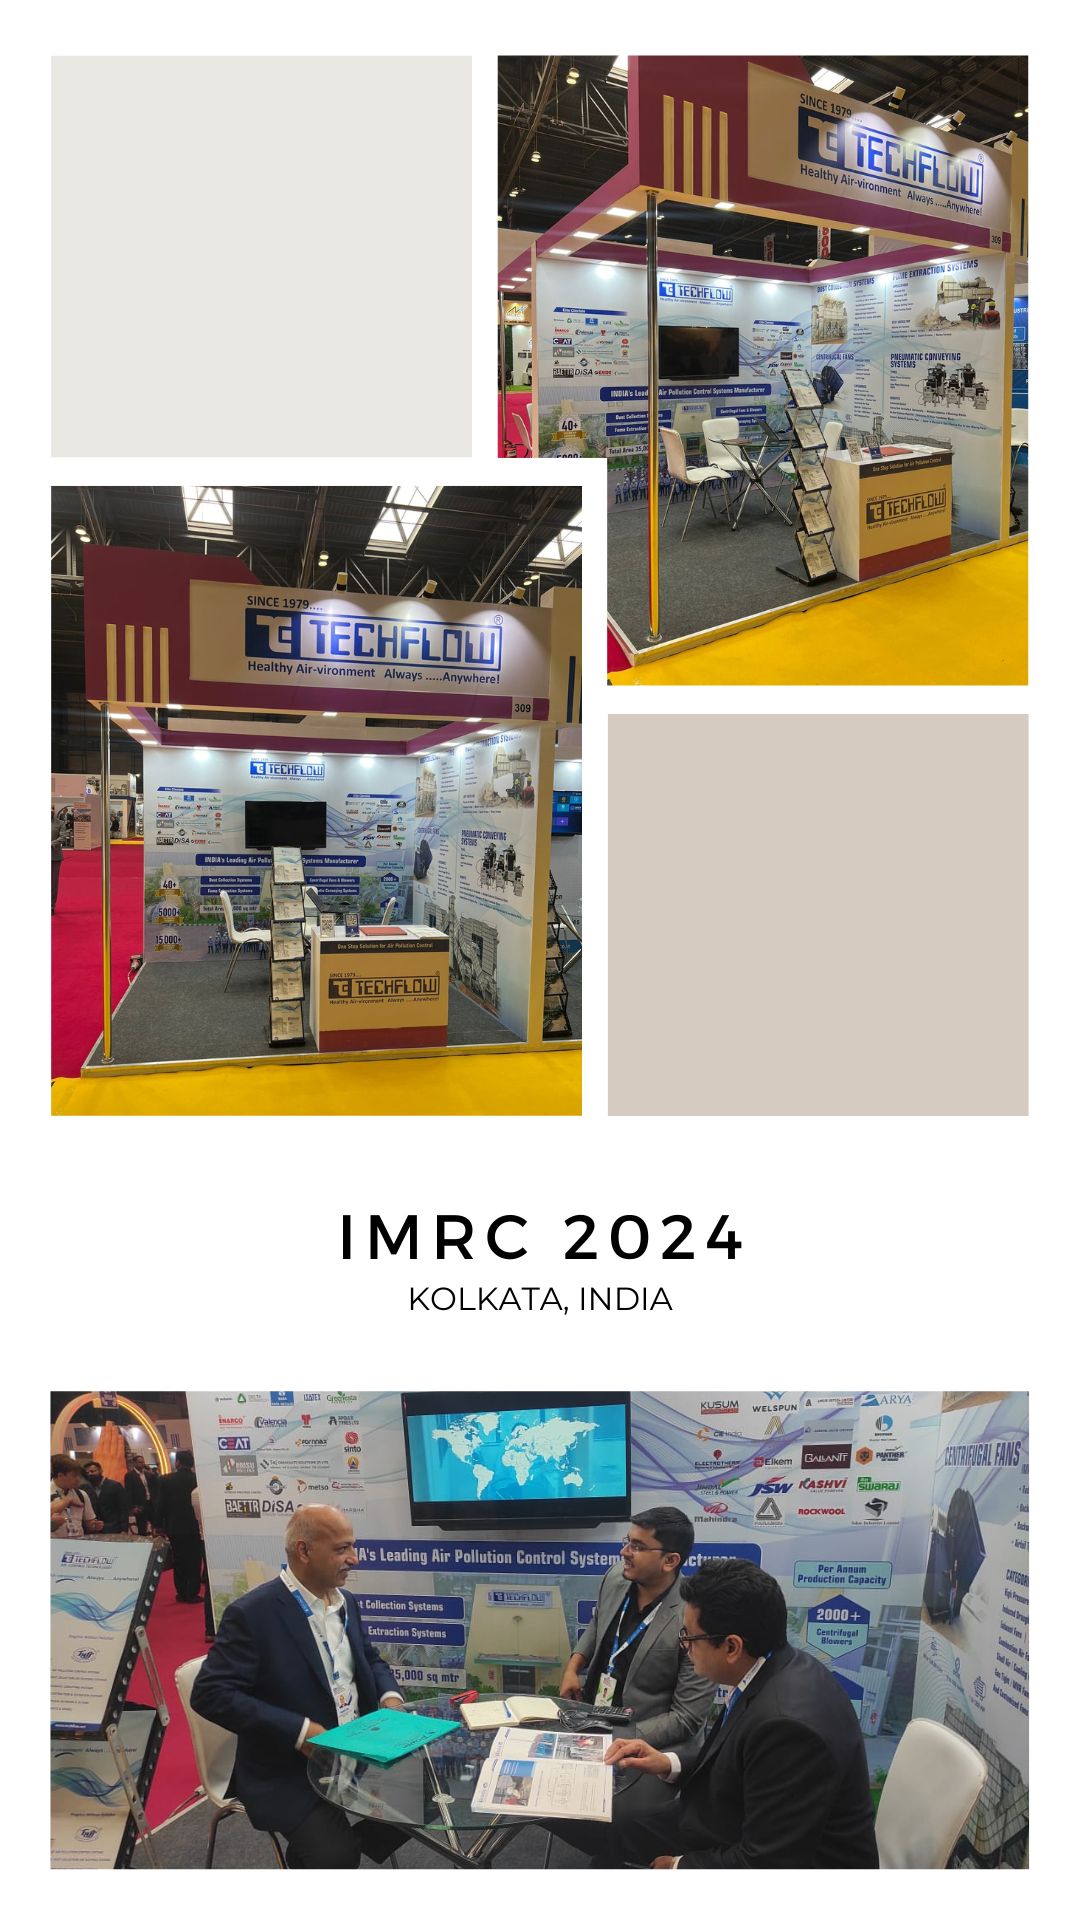
TECHFLOW was proud to participate in the 11th IMRC 2024 Convention & Exposition held in Kolkata from 23rd to 25th January 2024. At Booth 309, we showcased our comprehensive range of air pollution control solutions designed specifically for the material recycling industry, including dust collection systems, fume extraction systems, centrifugal blowers and fans, and pneumatic conveying systems. This event provided us with a valuable platform to connect with industry experts, share our latest innovations, and address the evolving needs of the recycling sector.
TECHFLOW, a leading provider of industrial air pollution control solutions, recently participated in the 11th IMRC 2024 Convention & Exposition, held in Hyderabad, India. The event provided a platform for TECHFLOW to showcase its innovative products and connect with industry professionals from the mining and mineral processing industry. This article will share our experience at the expo and express our gratitude to all attendees.
Showcasing Our Solutions
During the expo, TECHFLOW showcased its cutting-edge solutions for air pollution control in the mining and mineral processing industry, including:
- Pneumatic Conveying Systems: These systems efficiently transport materials like minerals, ores, and powders, reducing dust and spillage.
- Industrial Blowers and Fans: These powerful devices, including centrifugal fans, ensure proper ventilation, air circulation, and material transport within mining and mineral processing facilities.
- Dust Collection Systems: Our advanced dust collection systems capture and remove fine particles, ensuring cleaner air and improving working conditions.
- Electrostatic Precipitators: These systems effectively remove particulate matter from gas streams, enhancing air quality and complying with environmental regulations.
A Memorable Experience
The 11th IMRC 2024 was a resounding success for TECHFLOW. We were thrilled to interact with industry professionals, discuss their challenges, and provide tailored solutions. The event offered a unique opportunity to showcase our expertise and demonstrate our commitment to environmental sustainability and operational efficiency in the mining and mineral processing industry.
We were impressed by the level of interest and engagement from the attendees. Many visitors expressed their appreciation for our innovative products and our dedication to providing high-quality solutions.
A Heartfelt Thank You
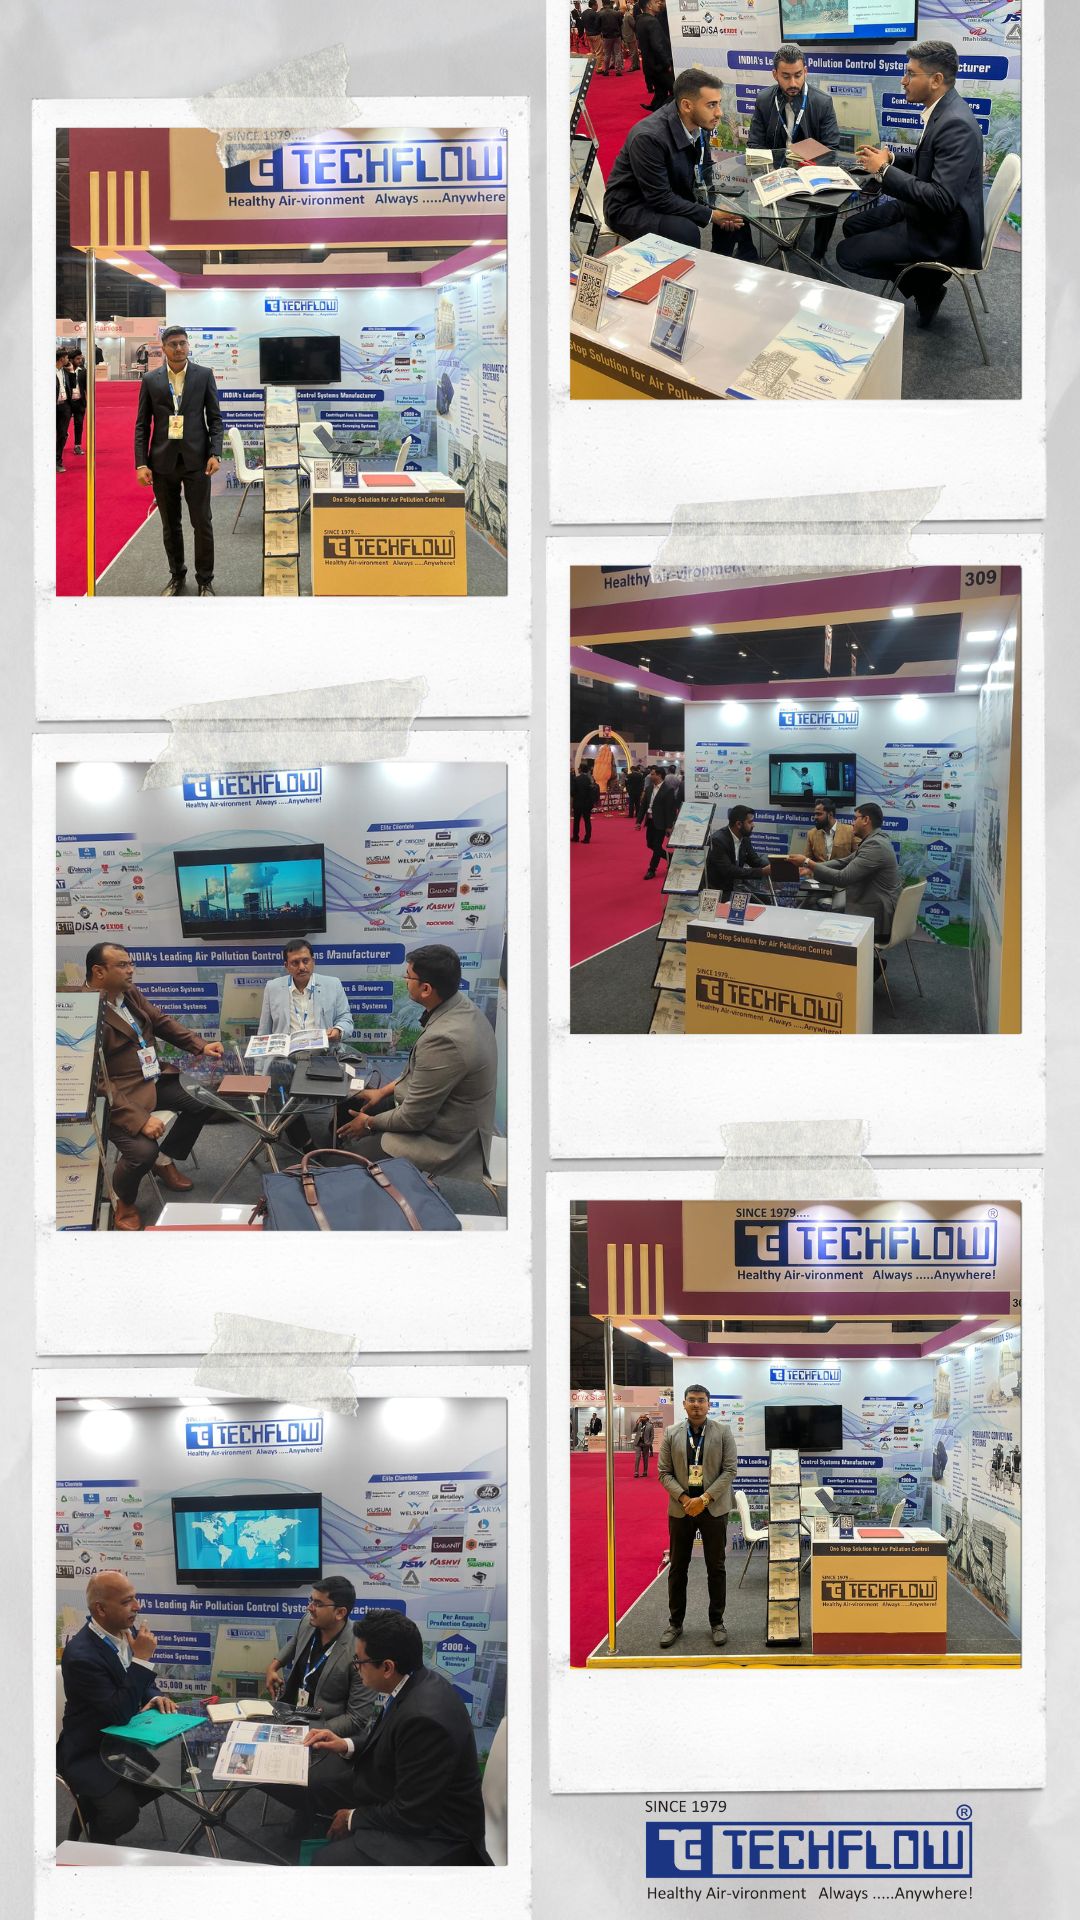
We would like to express our sincere gratitude to everyone who visited our booth at the 11th IMRC 2024. Your support and encouragement mean a lot to us. We are committed to continuing our efforts in developing advanced air pollution control solutions that meet the evolving needs of the mining and mineral processing industry.
Looking Ahead
TECHFLOW is excited about the future of air pollution control in the mining and mineral processing industry. We are dedicated to staying at the forefront of technological advancements and providing innovative solutions to address the challenges faced by mining and mineral processing operations worldwide.
We look forward to future opportunities to collaborate with industry professionals and contribute to a cleaner and healthier environment.
Key Benefits of TECHFLOW's Solutions for the Mining and Mineral Processing Industry:
- Improved Air Quality: Our solutions help reduce emissions of particulate matter, nitrogen oxides, and other pollutants, leading to cleaner air and better environmental impact.
- Enhanced Energy Efficiency: Our energy-efficient fans and blowers minimise energy consumption, reducing operating costs.
- Optimized Production Processes: Our air pollution control solutions improve the efficiency of mining and mineral processing operations, leading to increased productivity.
- Reduced Maintenance Costs: Our robust and reliable equipment requires minimal maintenance, saving time and money.
- Compliance with Environmental Regulations: Our solutions help mining and mineral processing operations comply with stringent environmental regulations and industry standards.
TECHFLOW's Commitment to Customer Satisfaction
At TECHFLOW, we are committed to providing exceptional customer service and support. Our team of experts is dedicated to understanding your specific needs and providing tailored solutions. We offer a wide range of services, including:
- Customized Design and Engineering: We work closely with our customers to design and engineer custom solutions that meet their unique requirements.
- Installation and Commissioning: Our experienced technicians ensure seamless installation and commissioning of our equipment.
- After-Sales Support: We provide comprehensive after-sales support, including maintenance, repair, and spare parts.
TECHFLOW's Commitment to Sustainability
TECHFLOW is committed to sustainable practices and environmental responsibility. We design and manufacture our products with a focus on energy efficiency, reduced emissions, and minimal environmental impact. By choosing TECHFLOW, mining and mineral processing operations can contribute to a more sustainable future.
TECHFLOW's Global Presence
TECHFLOW has a strong global presence, with customers in countries such as India, Europe, the Middle East, and Asia. Our experienced team can provide customized solutions to meet the specific needs of mining and mineral processing operations in different regions.
TECHFLOW's Expertise in Mining and Mineral Processing Ventilation
TECHFLOW offers comprehensive air handling solutions for mining and mineral processing facilities, including fans for ventilation, dust control, and material handling. Our fans are designed to optimize air flow, improve energy efficiency, and reduce noise pollution.
TECHFLOW's Focus on Innovation
TECHFLOW is constantly innovating to develop new and improved products. We invest heavily in research and development to stay at the forefront of technology and provide cutting-edge solutions to our customers.
TECHFLOW's Commitment to Quality
Quality is a cornerstone of TECHFLOW's business. We are committed to delivering high-quality products and services that meet or exceed industry standards. Our products are manufactured using state-of-the-art technology and rigorous quality control processes.
Thank you once again for your support and for making the 11th IMRC 2024 a memorable experience